Specialized Water Treatment Chemicals
High-purity synthetic polymers and chemical agents designed for scale inhibition and sewage treatment.
Benzalkonium Chloride(Dodecyl Dimethyl Benzyl ammonium Chloride)
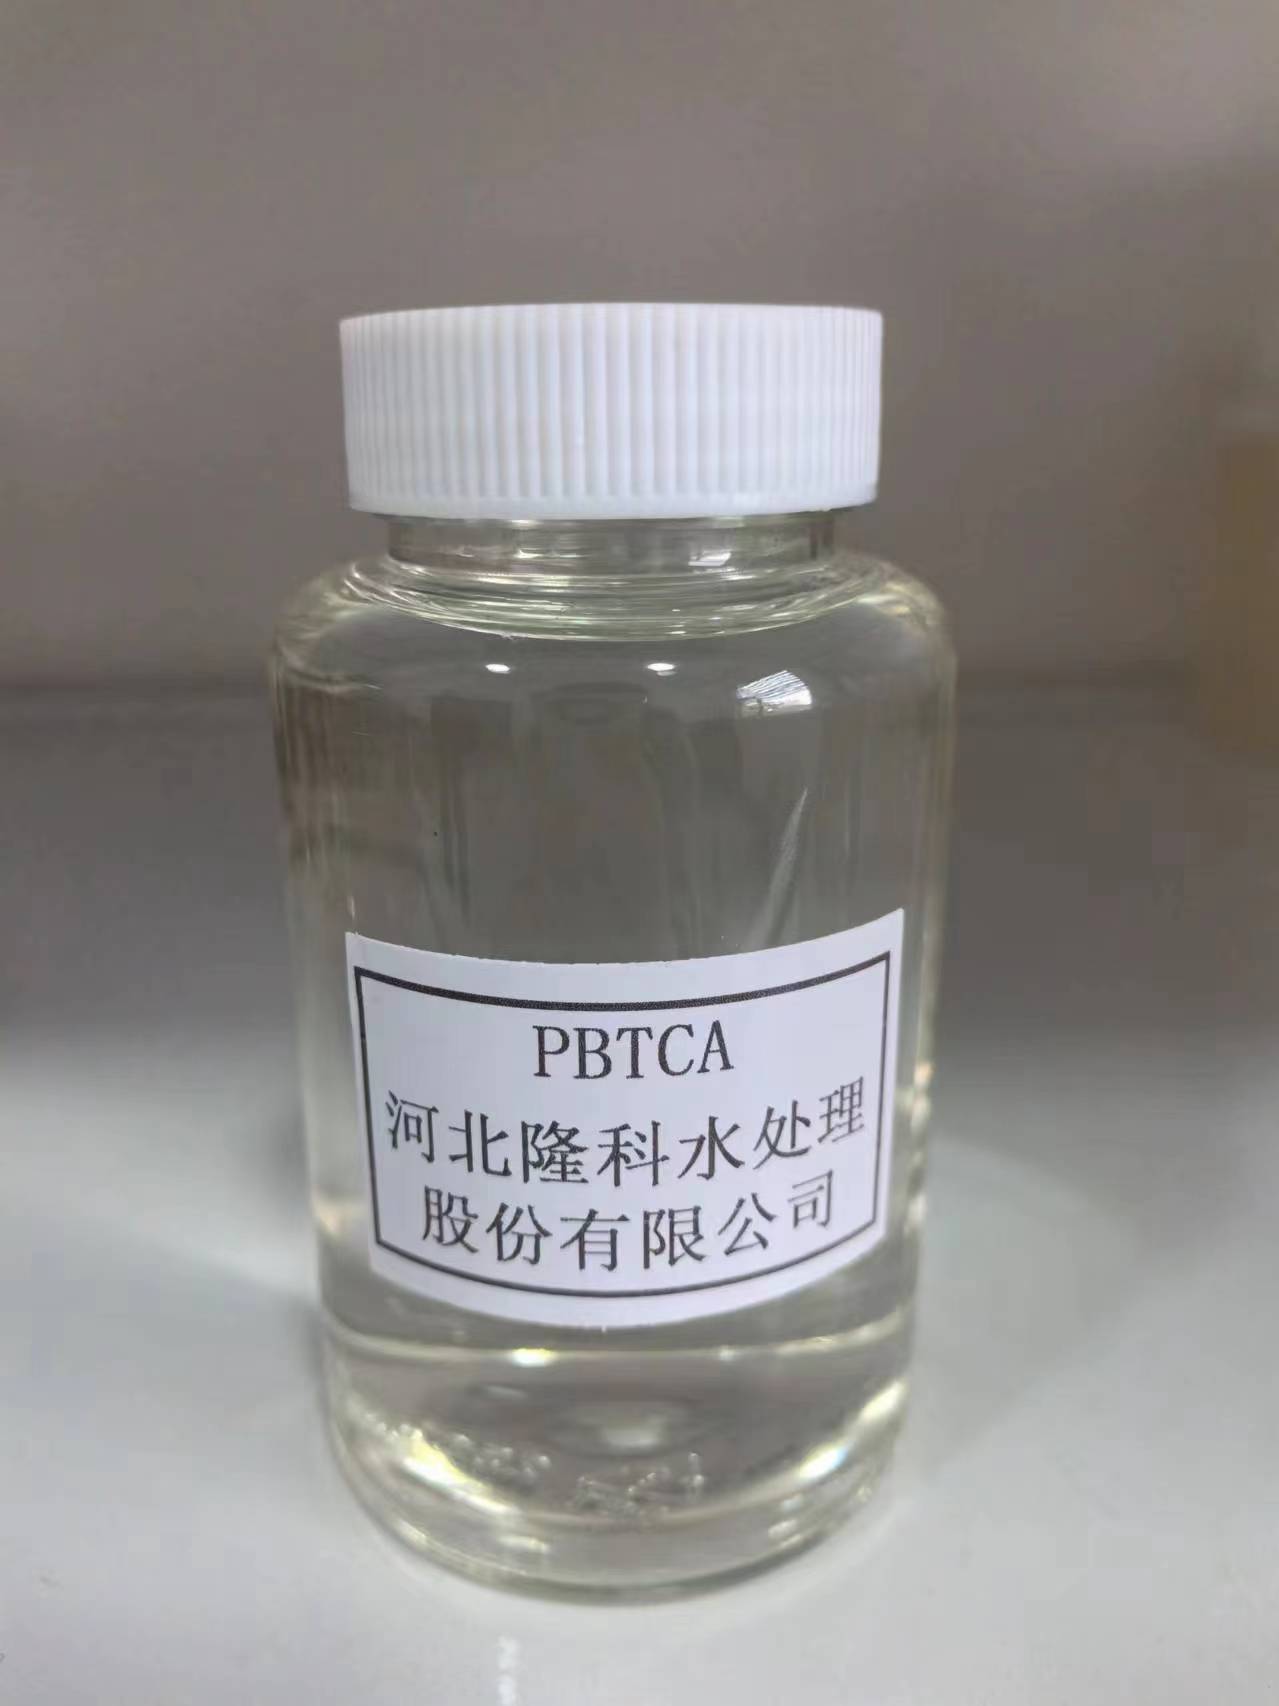
2-Phosphonobutane -1,2,4-Tricarboxylic Acid(PBTC)
Ethylene Diamine Tetra (Methylene Phosphonic Acid)EDTMPA(Solid)
Market Analysis
Water Treatment Landscapes in North America - Cuba
Addressing the intersection of industrial growth and environmental preservation in the Caribbean region.
Multi-Industry
Application Scope
High-Stability
Polymer Performance
Rapid-Action
Flocculation Rate
Global-Standard
Quality Control
In North America - Cuba, industrial facilities operating in refining and power generation face unique challenges due to high humidity and specific mineral compositions in local water sources. This necessitates the use of a robust chemical antiscalant to prevent mineral buildup in cooling systems, which can otherwise lead to significant energy losses and equipment downtime.
The regional focus has shifted toward sustainable wastewater management, driving the demand for efficient flocculant agents that can handle complex industrial effluents while meeting local environmental guidelines.
Procurement decisions in the Cuban industrial sector are increasingly driven by the balance between initial chemical cost and long-term operational efficiency. The ability of a dispersant to maintain system stability under varying load conditions is a critical metric for plant managers.
As the industry evolves, there is a growing preference for integrated solutions that combine scale inhibition with corrosion protection to extend the lifecycle of expensive industrial assets.
Evolution of Water Chemistry
Development Trajectory of Specialty Chemicals
From basic inorganic salts to high-performance synthetic polymers.
Early Stage
Basic Precipitation
Reliance on simple alum and lime for basic water clarification.
Growth Stage
Polymer Adoption
Introduction of polyacrylic acid and early organic dispersants.
Optimization
Chelation Focus
Development of specific chemical chelating agent for heavy metal removal.
Modern Era
High-Performance
Deployment of modified polymers like HPMA for extreme conditions.
Current Stage
Eco-Efficiency
Focus on biodegradable and low-phosphorus water treatment agents.
Future Strategic Directions
01
Technical Precision
Shift towards tailored molecular weights in polymers to match specific contaminant profiles in local Cuban water.
02
Regulatory Compliance
Increasing demand for chemicals that reduce the environmental footprint of industrial discharge.
03
Operational Integration
Combining chemical treatment with real-time monitoring to optimize dosing and reduce waste.
Strategic Outlook
Industrial Trends in Speciality Chemical Manufacturing
How technological shifts are redefining water treatment efficiency.
Molecular Optimization
Enhancing the stability of HPMA polymers to withstand higher temperature fluctuations in cooling towers.
User-Centric Dosing
Development of easier-to-handle chemical forms to reduce dosing errors in remote industrial sites.
Circular Economy
Designing chemicals that facilitate the recovery of water for reuse within the plant loop.
Synergistic Effects
Creating chemical blends that act as both scale inhibitors and corrosion preventatives.
The technical evolution in the specialty chemical sector is moving away from "one size fits all" products toward precision chemistry. By analyzing the specific ion concentration in the water of North America - Cuba, manufacturers can now adjust the functional groups of polymers to ensure maximum efficiency.
From a commercial perspective, the shift is toward "Performance-as-a-Service," where the focus is not just on the volume of chemicals sold, but on the measurable reduction of scale buildup and the extension of equipment lifespan.
Practical Applications
Local Implementation Scenarios in North America - Cuba
Solving real-world water challenges across diverse industrial sectors.
01
Sugar Refining Process Water
Using specialized flocculants to clarify process water and remove organic impurities in Cuban sugar mills to improve sucrose recovery.
02
Thermal Power Plant Cooling
Applying hpma polymer to prevent calcium carbonate scale in heat exchangers, ensuring stable energy output for the national grid.
03
Chemical Fertilizer Production
Utilizing chelating agents to manage metal ion concentrations in production loops, preventing catalyst poisoning and equipment corrosion.
04
Municipal Sewage Treatment
Implementation of high-efficiency dispersants to optimize sludge thickening and reduce the volume of waste for landfill disposal.
05
Petrochemical Refining Cooling Loops
Integrated use of chemical antiscalants and corrosion inhibitors to maintain the integrity of high-pressure piping systems in refinery environments.
Corporate Profile
About Hebei Longke Water Treatment Co., Ltd.
A modern joint-stock enterprise integrating scientific research, production, and technical service.
Strategic Core
R&D Foundation
Established a specialized chemical analysis and instrument room to provide routine water quality analysis and dynamic simulation experiments.
Product Diversification
Expanded the portfolio to include high-performance scale inhibitors, corrosion inhibitors, detergents, and flocculants.
Market Growth
Global Reach
Worldwide Distribution
Developed a global sales network, providing quality water treatment solutions to industries worldwide with a commitment to "quality first."
Comprehensive Water Treatment Catalog
Explore our full range of specialty chemicals for industrial water management.
Expert Q&A
Frequently Asked Questions
Technical insights regarding specialty chemicals and their application.
HPMA (Hydroxymethylene phosphonic acid) polymer acts as a powerful scale inhibitor and dispersant. It prevents the precipitation of calcium and magnesium salts on heat-exchange surfaces, maintaining thermal efficiency and reducing the frequency of acid cleaning.
Due to the specific water hardness and organic content in many Cuban industrial zones, standard chemicals may fail. High-performance dispersants ensure that particles remain suspended in the water, preventing sludge buildup in pipelines and cooling towers.
The choice depends on the charge of the particles in the wastewater (cationic, anionic, or non-ionic). It is recommended to perform a jar test using local water samples to determine the optimal molecular weight and charge density for maximum clarification.
You should focus on the stability constant of the metal-chelate complex, the pH range of effectiveness, and the solubility of the agent. For heavy metal removal, the selectivity of the chelating agent for the target ion is the most important factor.
The company provides comprehensive technical services, including routine water quality analysis, stable static screening for circulating cooling water, and dynamic simulation experiments to ensure the chosen product matches the actual operational environment.
A transition is necessary when you observe recurring scale buildup despite standard dosing, or when moving toward high-cycle water systems to reduce blowdown and save water. Consulting with a technical expert can help identify the exact tipping point.
Optimize Your Industrial Water Management in North America - Cuba
Partner with Hebei Longke Water Treatment Co., Ltd. for professional-grade chemicals and customized technical solutions tailored to your specific manufacturing needs.
Get a Custom Quote Today