Advanced Specialty Chemical Agents
Providing high-performance chemical solutions to enhance industrial efficiency and environmental compliance for Rwandan enterprises.
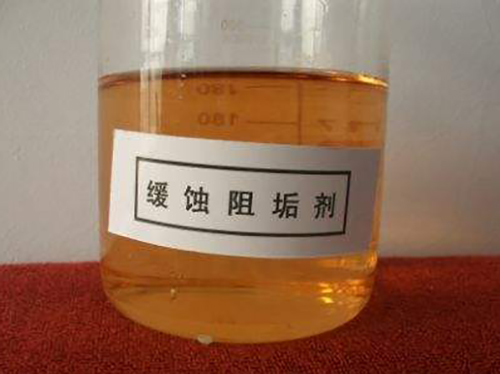
LK-319 Scale and Corrosion Inhibitor for Iron & Steel Plant
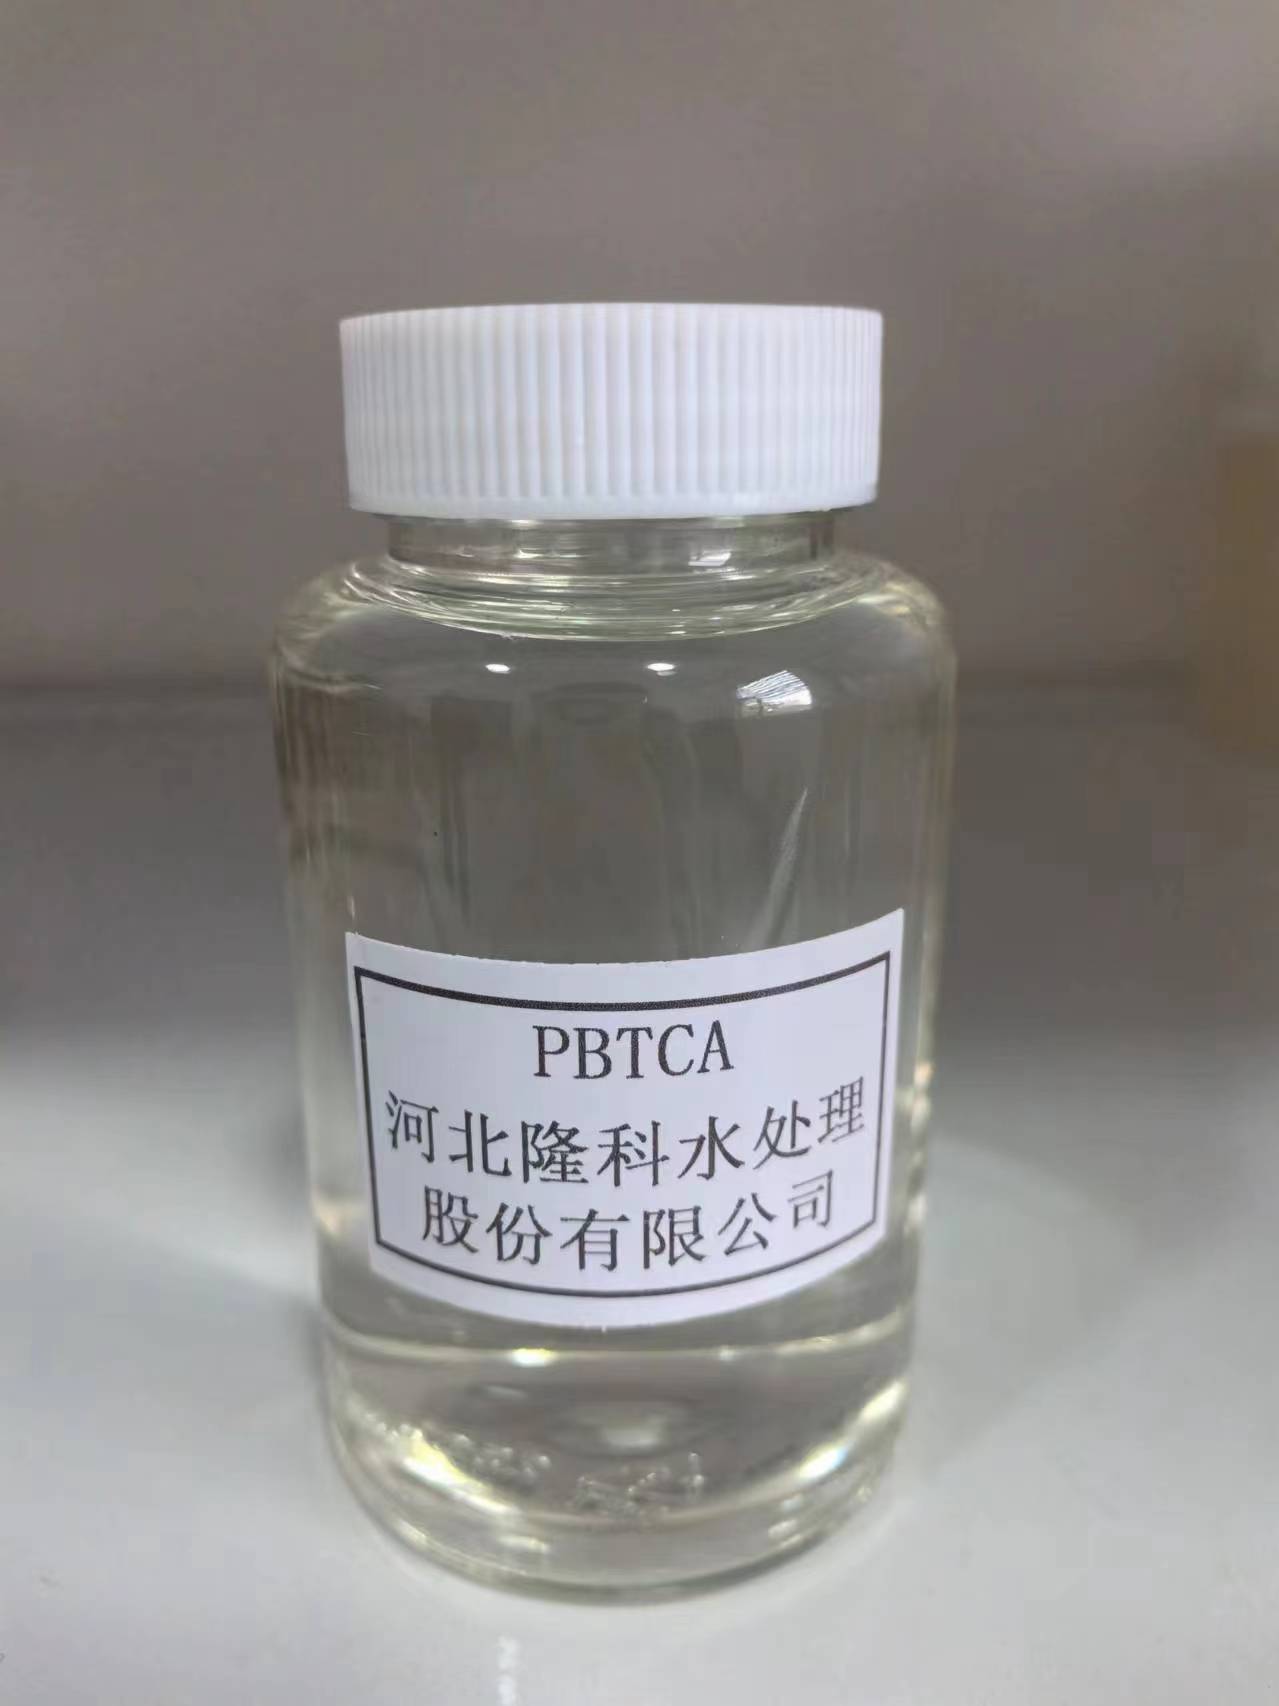
2-Phosphonobutane -1,2,4-Tricarboxylic Acid(PBTC)
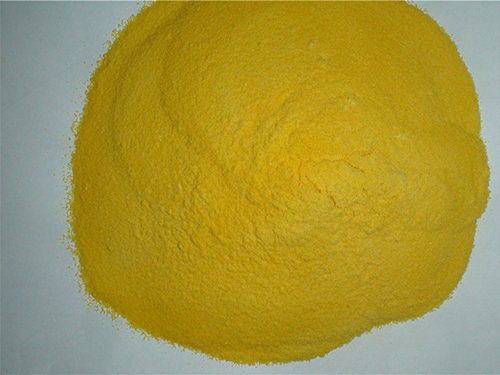
PAC Poly Aluminum Chloride
Water Treatment Challenges in Rwanda's Manufacturing Sector
Addressing the critical need for sustainable industrial water management.
In Rwanda, the rapid growth of the manufacturing and agri-processing sectors has increased the demand for sophisticated water treatment. Local industries often struggle with mineral scaling and organic pollutants in their cooling and process water. The integration of a high-quality dispersant is becoming essential to prevent deposits that reduce heat exchange efficiency and increase energy costs in industrial boilers.
Operating environments in the region frequently face fluctuations in water quality, necessitating the use of a robust chemical antiscalant. Without proper chemical intervention, equipment longevity is compromised by calcium and magnesium precipitates. Rwandan companies are increasingly shifting toward specialized chemical agents that offer higher stability under varying temperature and pH conditions to maintain continuous production cycles.
As environmental regulations tighten across East Africa, the focus has shifted toward efficient sewage treatment. The implementation of a precise chemical chelating agent helps in removing heavy metals and complex ions from industrial effluent. This transition not only ensures regulatory compliance but also opens opportunities for water recycling, reducing the overall operational footprint of factories in Rwanda's industrial zones.
Evolution of Industrial Chemical Applications
From basic filtration to advanced molecular polymer technology.
Development Path
Early Stage
Basic Coagulation
Reliance on simple inorganic salts for water clarification with low selectivity and high sludge production.
Growth Phase
Polymer Introduction
Introduction of organic polymers like hpma polymer to improve scale inhibition and dispersion.
Modern Era
Specialized Synthesis
Development of multi-functional chelants and tailored flocculants for specific industrial effluent profiles.
Technological Shifts
- Biodegradable Agents Shift toward phosphorus-free and biodegradable polymers to minimize environmental impact.
- Precision Dosing Integration of automated sensor-based dosing systems to reduce chemical waste and costs.
- Synergistic Formulations Combining antiscalants and corrosion inhibitors in a single high-stability product.
Future Trajectories in Water Chemistry
Analyzing the drivers of efficiency and sustainability in chemical manufacturing.
Technical Optimization
Enhancing molecular weight and charge density in polymers to achieve faster settling rates in wastewater treatment.
Operational Cost Control
Focusing on high-concentration formulations to reduce shipping costs and storage requirements for remote sites.
Application Diversification
Adapting water treatment chemicals for use in textile dyeing, mining, and food processing plants.
Quality Standardization
Implementation of global standards to ensure consistency in batch production and predictable performance.
The growth of Rwanda's industrial sector provides significant room for the adoption of customized chemical solutions. As factories upgrade their machinery, the need for high-purity chemical agents will likely increase, shifting the market from generic supplies to engineered solutions.
Supply chain resilience remains a priority. Local enterprises are seeking partners capable of providing technical support and stable delivery, ensuring that water treatment processes are not interrupted by logistical delays.
Industrial Application Scenarios in Rwanda
Practical deployment of water treatment chemicals across diverse sectors.
1
Food and Beverage Processing
Using high-grade flocculants to treat organic-rich wastewater from breweries and dairies, ensuring effluent meets Rwanda's environmental discharge standards.
2
Industrial Cooling Towers
Implementing antiscalants to prevent mineral buildup in cooling systems of power plants and factories, significantly reducing maintenance downtime.
3
Textile Manufacturing
Applying chelating agents to sequester metal ions from dyeing baths, improving color consistency and treating toxic wastewater before disposal.
4
Municipal Sewage Plants
Deploying large-scale polymer flocculants to accelerate sludge sedimentation in urban wastewater facilities, increasing the capacity of treatment plants.
5
Chemical Production Facilities
Utilizing specialized dispersants in the manufacturing of other chemicals to maintain suspension stability and prevent piping blockages.
Brand Story
Hebei Longke Water Treatment Co., Ltd. Global Development Journey
Establishment
Founding and Research
Established as a modern joint-stock enterprise integrating scientific research, production, and service in Hebei Province.
Infrastructure
Facility Expansion
Developed dedicated chemical analysis and instrument rooms to provide routine water quality analysis and dynamic simulation experiments.
Market Growth
Domestic Leadership
Expanded product reach across 18 provinces in China, serving refineries, power plants, and steel mills.
Global Reach
International Export
Successfully expanded sales worldwide, providing high-quality scale inhibitors and sewage treatment agents to global markets.
Quality Commitment
Quality-First Principle
Consistent focus on "Quality First," earning praise from global customers through sincere service and reliable products.
Future Vision
Sustainable Innovation
Continuing to develop advanced benzylphosphonic acid and other eco-friendly water treatment solutions for the global industry.
Specialized Water Treatment Product Portfolio
A comprehensive range of chemical agents designed for scale inhibition, corrosion protection, and efficient sludge removal.
Technical Support and FAQ
Expert answers regarding the application of specialty chemicals in Rwanda.
What are the technical specifications for high-performance flocculants in industrial use?
Our flocculants are engineered with specific molecular weights and charge densities to suit different water types. Technical data sheets provide details on viscosity, solubility, and active content to ensure optimal performance in various Rwandan industrial effluents.
How should a chemical antiscalant be dosed in cooling water systems?
Dosing should be based on a water quality analysis. We recommend initial jar tests to determine the minimum effective concentration, followed by continuous dosing via a metering pump to maintain a stable concentration of the antiscalant in the circulating water.
How does the quality of hpma polymer affect scale inhibition?
The purity and polymerization degree of hpma polymer directly impact its ability to distort crystal growth of calcium carbonate. High-quality polymers provide superior dispersion and prevent the formation of hard scale on heat exchange surfaces.
Are these chemical chelating agents compatible with other water treatment additives?
Most of our chelating agents are designed for compatibility. However, we suggest a compatibility test to avoid precipitation when mixing anionic and cationic polymers. Our technical team can provide guidance on the correct sequence of chemical addition.
What is the typical shelf life and storage requirement for industrial dispersants?
Our industrial dispersants typically have a shelf life of 12 to 24 months when stored in original sealed containers. They should be kept in a cool, dry, and well-ventilated area, away from strong oxidizers and direct sunlight.
What is the ROI when switching to advanced specialty water chemicals?
The return on investment is realized through reduced energy consumption (due to cleaner heat exchangers), extended equipment lifespan, and lower wastewater treatment costs. Many Rwandan clients see a decrease in overall maintenance expenditure within the first year.
Optimize Your Industrial Water Systems in Rwanda
Leverage Hebei Longke's global expertise and high-performance chemical agents to ensure operational efficiency and environmental compliance. Partner with a quality-first supplier for your water treatment needs.
Request Technical Consultation