Specialized Chemical Agents for Water Management
Advanced chemical formulations to optimize industrial cooling and wastewater processing in Morocco.
Acrylic Acid-2-Acrylamido-2-Methylpropane Sulfonic Acid Copolymer (AA/AMPS)
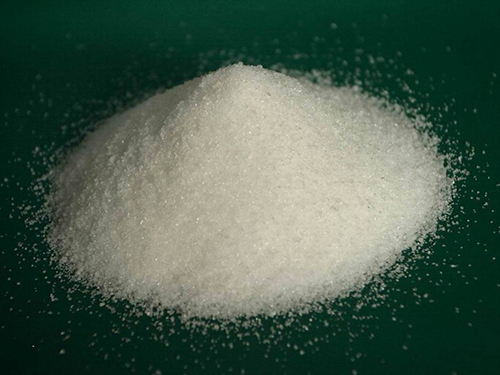
Tetra Sodium of 1-Hydroxy Ethylidene-1,1-Diphosphonic Acid HEDP·Na4(Granule)
Isothiazolinones (CMIT/MIT)
Analyzing Water Treatment Challenges in the Moroccan Industrial Sector
Optimizing chemical selection based on regional environmental and operational constraints.
Morocco's unique geography, characterized by varied mineral content in groundwater and high evaporation rates in arid regions, often leads to rapid mineral buildup in industrial cooling systems. This necessitates the use of a robust chemical antiscalant to maintain heat exchange efficiency and prevent costly downtime.
Local industrial operators in refining and phosphate processing face significant challenges with suspended solids and colloidal impurities. The application of a high-grade flocculant is essential for accelerating sedimentation and improving the quality of reclaimed water, supporting local sustainability goals.
Procurement in the Moroccan market is increasingly shifting toward specialized polymers. The adoption of an hpma polymer allows facilities to handle higher hardness levels in circulating water, reducing the frequency of blowdowns and lowering overall water consumption.
Evolution of Speciality Chemical Applications
Tracing the transition from basic water treatment to advanced polymer science.
Development Trajectory
-
Early Adoption Stage
Reliance on basic inorganic salts for coagulation and simple pH adjustment to manage mineral deposits. -
Polymerization Stage
Introduction of synthetic polymers, including the use of a dispersant, to prevent particle aggregation and improve scale inhibition. -
Current Optimization Stage
Integration of multi-functional agents and tailored molecular weights to meet specific industrial water chemistry requirements.
Future Strategic Trends
- Sustainability — Shifting toward biodegradable chelating agents to reduce the environmental footprint of industrial effluent.
- Customization — Developing site-specific formulations that adapt to the varying salinity of regional water sources.
- Energy Efficiency — Using high-efficiency antiscalants to reduce the energy required for pumping and heat exchange.
Future Directions in Industrial Water Chemistry
Four critical dimensions shaping the next generation of water treatment solutions.
Material Science
Advanced development of HPMA-based polymers to withstand higher temperatures and extreme pH levels.
Resource Recovery
Enhanced use of a chemical chelating agent to selectively recover valuable metals from industrial waste.
Operational Cost
Reducing chemical dosage through precision dosing systems and higher-concentration active ingredients.
Environmental Compliance
Alignment with international standards for phosphorus-free water treatment chemicals.
Industry Outlook for the Maghreb Region
Over the next few years, the industrial landscape in Morocco is expected to prioritize water circularity. This will drive demand for more efficient flocculants and dispersants that allow for the reuse of process water without compromising equipment integrity.
From a commercial perspective, the integration of technical services—such as water quality analysis and simulation experiments—will become a key differentiator for suppliers providing specialized chemicals to the power and chemical fertilizer industries.
Implementation Scenarios for Water Treatment Chemicals
Practical applications across various industrial environments in Morocco.
1
Power Plant Cooling Towers
Using an HPMA polymer combined with a chemical antiscalant to prevent calcium carbonate scaling in high-cycle cooling systems, ensuring optimal thermal conductivity.
2
Phosphate Mining Effluent
Deploying specialized flocculants to separate fine mineral particles from wastewater, enabling the rapid clarification of large volumes of process water.
3
Chemical Fertilizer Production
Implementing a chemical chelating agent to manage metal ion concentrations in production lines, preventing precipitation and equipment corrosion.
4
Industrial Boiler Feedwater
Applying a high-efficiency dispersant to keep sludge and scale-forming minerals in suspension, preventing deposits on boiler tubes.
5
Municipal Sewage Treatment
Utilizing organic flocculants for the removal of organic matter and suspended solids, improving the efficiency of secondary clarification stages.
Commitment to Water Treatment Excellence
Hebei Longke Water Treatment Co., Ltd. integrates scientific research, production, and technical services.
Foundation
Company Establishment
Integrated Industrial Foundation
Established as a modern joint-stock enterprise combining research, production, and service, located in the Neiqiu county Industrial Zone.
Capability
Technical Advancement
Development of Analysis Infrastructure
Creation of specialized chemical analysis and instrument rooms to provide routine water quality analysis and dynamic simulation experiments.
Growth
Market Expansion
Global Reach and Diversification
Expanding product lines to include scale inhibitors, corrosion inhibitors, and sewage treatment agents, serving diverse industries worldwide.
Chemical Solutions for Moroccan Industrial Water Requirements
A comprehensive portfolio of specialized agents for scale prevention, dispersion, and clarification.
Industrial Water Treatment FAQ
Technical and procurement guidance for the Moroccan manufacturing sector.
How do I choose the right flocculant for industrial wastewater in Morocco?
The choice depends on the charge and size of the suspended particles. We recommend conducting a jar test using local water samples to determine the optimal molecular weight and charge density required for effective coagulation and sedimentation.
What are the benefits of using HPMA polymer over traditional antiscalants?
HPMA polymer offers superior thermal stability and higher tolerance to water hardness. It effectively inhibits the growth of calcium carbonate crystals even in high-temperature environments, reducing the overall chemical consumption.
Can a chemical chelating agent prevent corrosion in industrial piping?
Yes, by sequestering metal ions that would otherwise act as catalysts for corrosion or form scale, chelating agents help maintain a protective environment within the piping system, extending the equipment's operational lifespan.
How does a dispersant improve the efficiency of cooling towers?
Dispersants prevent the aggregation of fine particles and mineral precipitates. By keeping these solids in suspension, they prevent the formation of a sludge layer on heat exchange surfaces, ensuring maximum heat transfer efficiency.
What technical support is available for Moroccan industrial clients?
Hebei Longke Water Treatment Co., Ltd. provides routine water quality analysis and dynamic simulation experiments to ensure that the chemical dosage is optimized for the specific water chemistry of the client's facility.
What are the procurement considerations for imported water chemicals in Morocco?
Buyers should prioritize suppliers who can provide technical data sheets, stability certificates, and the ability to adjust formulations based on regional water analysis to ensure compatibility with local infrastructure.
Optimize Your Water Treatment Strategy in Morocco
Discuss your technical requirements and water quality challenges with our experts to identify the most efficient chemical solutions for your facility.
Contact Us Now